When Standard Punches Run Out of Space, Gooseneck Punches Make Room
Sep 10, 2026
When Standard Punches Run Out of Space,
Gooseneck Punches Make Room
Gooseneck Press Brake Punches for Deep Boxes, U-Channels and Return Flanges
In the first article of the Bendmax Common Press Brake Tools Series, we introduced the Standard Press Brake Punch as the versatile foundation of everyday bending.
A Standard Punch is strong, practical and suitable for many conventional bending operations. However, some workpieces create a different challenge: the problem is not bending force, but insufficient clearance.
Deep boxes, U-channels, return flanges and multi-bend enclosures can interfere with a conventional straight punch before the forming process is complete. When this happens, increasing the machine tonnage will not solve the problem.
The solution is often a different tool geometry.
When Standard Punches Run Out of Space, Gooseneck Punches Make Room.
1. What Is a Gooseneck Press Brake Punch?
A Gooseneck Punch is a specialized upper tool for a press brake. Its recessed, curved or offset profile creates additional clearance behind the punch tip.
This open area allows previously formed flanges and deep workpiece sections to move around the punch body without colliding with the tooling.
Compared with a conventional Standard Punch, a Gooseneck Punch is especially useful for:
Deep box bending
U-channel forming
Return flange bending
Electrical cabinet production
Enclosure and housing fabrication
Deep channels and pans
Multi-step bending operations
Parts with restricted internal clearance
The name comes from the tool’s characteristic neck-shaped profile. The geometry is designed to provide space where a straight punch would normally interfere with the workpiece.
Bednmax - Amada system press brake gooseneck/swan punch
Bednmax - Amada system press brake gooseneck/swan punch
Bednmax - WILA/Trumpf system press brake gooseneck/swan punch
Bednmax - Bystronic system press brake gooseneck/swan punch
2. Why Standard Punches Sometimes Run Out of Clearance
A Standard Punch has a relatively solid and robust body. This design provides good structural strength and makes it suitable for general-purpose bending.
However, during complex bending, the workpiece does not remain flat.
After the first bend, the flange rises. After several bends, the workpiece may begin to surround the upper tool. When the next flange moves upward, it can collide with the solid body of the Standard Punch.
Typical interference problems include:
A deep side wall hitting the punch body
A return flange colliding with the punch
A previously bent flange contacting the tool holder
A narrow box becoming too tight for a straight punch
A final bend becoming impossible because the part surrounds the tool
This is a clearance problem, not necessarily a strength problem.
Strength solves load problems. Geometry solves clearance problems.
A stronger Standard Punch may withstand more bending force, but it cannot create additional space around a deep or previously formed flange.
No. 11.660
Bednmax - Amada system press brake gooseneck/swan punch
No. 19.226
Bednmax - Wila system press brake gooseneck/swan punch
No.15.380
Bednmax - Trumpf system press brake gooseneck/swan punch
No.16. 500
Bednmax - Amada system press brake gooseneck/swan punch
3. How Gooseneck Geometry Creates Morepace
The main feature of a Gooseneck Punch is its recessed neck or throat.
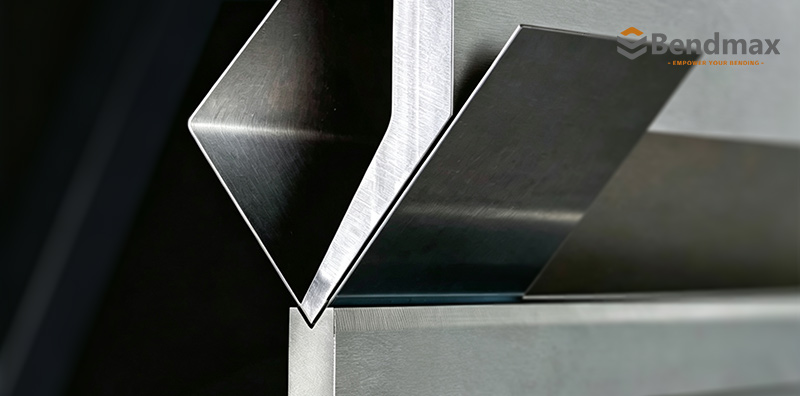
Instead of using a solid profile behind the punch tip, the tool removes material from the interference area. This creates a clearance zone where the workpiece flange can pass during the bending stroke.
The working principle is simple:
• The punch tip contacts the sheet metal.
• The material begins to form around the V-die.
• Previously bent flanges move upward.
• The recessed punch profile provides space for those flanges.
• The bend can be completed without the workpiece hitting the punch body.
This geometry is particularly valuable when forming deep boxes or return bends, where the workpiece becomes increasingly close to the upper tooling during successive operations.
4. Typical Applications of Gooseneck Punches
Deep Box Bending
Deep boxes are one of the most common applications for Gooseneck Punches.
When the first sides of a box have already been bent, the remaining flanges may rise beside the punch. A straight punch can collide with these walls before the final bend is completed.
The recessed profile of a Gooseneck Punch allows the existing box walls to move into the clearance area.
Typical products include:
• Electrical enclosures • Control cabinets • Metal housings • Machine covers
• Stainless steel boxes • Sheet metal pans • Industrial equipment frames
U-Channel Forming
U-channels often require tall side flanges and narrow internal spaces. A Standard Punch may not provide enough room for the side walls to rise.
A Gooseneck Punch offers additional clearance for forming deep channel profiles while reducing the risk of interference.
Return Flange Bending
Return flanges fold back toward the main body of the workpiece. This creates a restricted bending area that can be difficult to reach with a straight punch.
The recessed throat of a Gooseneck Punch allows the return flange to pass behind the working tip during forming.
Multi-Bend Components
Some components require several bends in different directions. As the part becomes more complex, previously formed flanges can interfere with the next bending operation.
Gooseneck tooling provides more freedom for the workpiece and can make difficult bending sequences easier to complete.
5. Gooseneck Punch vs. Standard Punch
Feature
Standard Punch
Gooseneck Punch
Main purpose
General-purpose bending
Clearance for complex profiles
Body design
Solid and robust
Recessed or offset
General bending
Excellent
Good
Deep box bending
Limited by clearance
Well suited
U-channel forming
Application dependent
Well suited
Return flanges
Limited in restricted spaces
Better access
Structural strength
Generally higher
Depends on throat depth and design
Best advantage
Strength and versatility
Additional workpiece clearance
The two tools are not direct replacements for each other.
A Standard Punch should normally be selected when the workpiece has conventional geometry and sufficient clearance. A Gooseneck Punch becomes useful when the workpiece physically interferes with the standard tool.
6. The Main Advantage: More Clearance
The greatest benefit of a Gooseneck Punch is not higher tonnage or a sharper bend angle.
Its main advantage is additional clearance.
This can help manufacturers:
Complete deeper bends
Reduce punch-to-workpiece interference
Form return flanges more easily
Improve access to narrow profiles
Reduce the need for special workpiece relief cuts
Simplify complex bending sequences
Improve production flexibility
For many deep-profile applications, the correct punch geometry can be more important than simply choosing a stronger tool.
Press Brake Gooseneck / Swan Punch
7. The Structural Trade-Off
The clearance created by a Gooseneck Punch comes from removing material from the punch body.
This means that a deeper throat may reduce the cross-sectional area supporting the working tip. As the throat becomes deeper, the punch may become
more sensitive to:
• Bending load
• Tool deflection
• Uneven loading
• Concentrated pressure
• Incorrect punch length
• Excessive forming force
• Improper die selection
For this reason, a Gooseneck Punch should not be selected only by its appearance or throat depth.
The required clearance must be balanced with:
• Material thickness
• Material type
• Required inside radius
• Box or flange depth
• Bending length
• Punch angle
• V-die opening
• Machine tonnage
• Tooling load rating
• Actual bending method
A Gooseneck Punch is designed to create space, but it still needs sufficient structural strength for the application.
8. Why Throat Depth Matters
The throat depth determines how much space is available behind the punch tip.
A shallow throat may be suitable for:
• Short return flanges
• Moderate box depths
• Small channels
• General clearance improvement
A deeper throat may be required for:
• Tall box walls
• Deep U-profiles
• Long return flanges
• Enclosures with restricted internal dimensions
• Complex multi-bend parts
However, more throat depth is not always better. A very deep recess can reduce tool rigidity and may limit the allowable bending load.
The correct approach is to select the minimum throat depth that provides the required clearance, while maintaining sufficient strength and stability.
9. Gooseneck Punches and Box Bending Sequence
Tool selection is only one part of successful box bending. The bending sequence also affects clearance.
For many box-shaped components, operators should consider bending the shorter flanges first. This can help preserve access for the later bends and reduce the risk of surrounding the punch with previously formed walls.
Before production, check:
The height of each flange
The distance between opposite walls
The punch throat depth
The punch segment length
The tool holder dimensions
The machine daylight
The position of the final bend
The possibility of corner interference
For narrow or fully enclosed boxes, segmented tooling or special horn sections may also be required. A single Gooseneck Punch cannot solve every horizontal or corner-clearance problem.
10. Gooseneck Punches Are Not a Universal Solution
Although Gooseneck Punches provide more clearance, they do not eliminate every bending limitation.
A Gooseneck Punch may not be suitable when:
The required bending load is too high
The throat depth is insufficient
The box is deeper than the available machine clearance
The tool is too long for the required load
The workpiece requires clearance at both punch ends
The part needs a special offset or horn profile
The selected V-die does not match the application
In these situations, the solution may involve:
Segmented Gooseneck Punches
Provide greater flexibility for complex parts and localized clearance requirements.
Horn Punches
Useful for reaching narrow or enclosed areas that require additional access around the punch.
Sash Punches
A narrow punch with an angled tip, suitable for tight bending areas and restricted profiles.
Window Punches
Designed for specific clearance requirements around previously formed sections or enclosed profiles.
Custom forming tools
Specially designed when standard punch geometries cannot meet the workpiece requirements.
A different bending sequence
Whatever you needs, CARESTONE is at your side.
A press brake with greater daylight
More machine opening space may be required for very deep or complex workpieces.
A lower forming force or alternative bending method
Adjusting the bending method can help when tooling clearance or load becomes a limitation.
The best tooling choice depends on the complete workpiece geometry rather than on one dimension alone.
11. How to Choose the Right Gooseneck Punch
Before selecting a Gooseneck Punch, review the following information.
Workpiece Geometry
Provide the finished part drawing, especially the height and position of previously formed flanges.
Material and Thickness
Material type and thickness affect the required bending force, inside radius and tool load.
Required Clearance
Measure the distance between the bend line and the interfering flange or wall.
Punch Angle and Nose Radius
The punch angle and nose radius must match the required bending operation and the selected V-die.
Machine Capacity
Check the machine tonnage, bending length, daylight and clamping system before choosing the tool.
Load Rating
The allowable load of the Gooseneck Punch must be suitable for the actual application. Do not assume that the tool can use the full capacity of the press brake.
Tooling System
Confirm the press brake tooling interface, such as:
Amada system
Trumpf system
WILA system
Bystronic system
LVD system
12. Gooseneck Punches from Bendmax
Bendmax manufactures press brake punches and dies for standard and specialized bending applications.
Our Gooseneck Punch solutions are designed to provide:
Reliable Clearance
Recessed profiles create additional space for deep boxes, U-channels and return flanges.
Precision Geometry
Accurate machining and grinding help maintain consistent punch dimensions and forming performance.
Suitable Material Selection
Depending on the application, Bendmax tooling can be manufactured using materials such as C45 or 42CrMo.
Application-Based Customization
Different throat depths, punch angles, working heights and lengths can be considered according to the customer’s workpiece and machine requirements.
System Compatibility
Tooling can be supplied for commonly used press brake systems, subject to confirmation of the required interface and dimensions.
For custom Gooseneck Punches, customers can provide a part drawing, material thickness, bending angle, flange height and machine information. Bendmax can then evaluate the required clearance and recommend a suitable tooling design.
13. When Should You Choose a Gooseneck Punch?
A Gooseneck Punch is a strong option when:
A Standard Punch collides with the workpiece
The part has deep side walls
The workpiece includes long return flanges
A U-channel requires additional internal clearance
The bending sequence creates interference
The part becomes difficult to rotate or reposition
A conventional punch cannot reach the required bend line
The key question is not:
“Do I need a stronger punch?”
It is:
“Does the workpiece need more space around the punch?”
If the answer is yes, a Gooseneck Punch may be the right next step.
14. The Engineering Lesson
The Standard Press Brake Punch is the versatile foundation of everyday bending. But when deep profiles, return flanges or previously formed walls begin to interfere with the tooling, a different geometry is required.
A Gooseneck Press Brake Punch creates additional clearance behind the working tip, helping manufacturers form deep boxes, U-channels and return flanges more efficiently.
Its main advantage is clear:
A Standard Punch provides strength and versatility. A Gooseneck Punch provides the space needed for complex bending.
The correct choice should always balance clearance, tool strength, machine capacity and workpiece geometry.
In the next article of the Bendmax Common Press Brake Tools Series, we will explore another specialized punch profile and explain when it becomes more suitable than a conventional Gooseneck Punch.
15. The FAQs
The Standard Press Brake Punch is the versatile foundation of everyday bending. But when deep profiles, return flanges or previously formed walls begin to interfere with the tooling, a different geometry is required.
A Gooseneck Press Brake Punch creates additional clearance behind the working tip, helping manufacturers form deep boxes, U-channels and return flanges more efficiently.
Its main advantage is clear:
1. Can you manufacture custom press brake tooling?
Yes. Bendmax manufactures custom press brake punches, dies and tooling based on your drawings, dimensions, material, thickness and bending requirements.
2. What information do you need for a quotation?
Please provide the tooling drawing or part drawing, press brake model, tooling system, material, thickness, bending angle, inside radius and required length. Photos or samples are also helpful.
3. What materials are used for your press brake tooling?
We commonly use C45 and 42CrMo, selected according to the tooling design and application requirements. Special material requirements can also be discussed.
4. What hardness does your tooling achieve?
Depending on the tooling design, the body is typically hardened to HRC 30–35, while the working area can achieve approximately HRC 54–60 for improved wear resistance and service life.
5. How do you ensure tooling accuracy?
We use precision CNC machining, grinding and inspection equipment to control dimensions, profile accuracy, straightness and hardness, with a typical tooling accuracy of up to ±0.02 mm.
6. What is your production lead time?
Lead time depends on the tooling type, quantity and customization requirements. Standard tooling can usually be supplied faster, while custom tooling requires additional engineering and production time.
7. Can you manufacture
Yes. We support OEM and bulk orders, including tooling manufactured according to customer drawings, specifications and required tooling systems.
8. Do you ship press brake tooling worldwide?
Yes. Bendmax supplies press brake tooling to customers worldwide and can support export packaging, shipping coordination and after-sales service.
9. Can you help me choose the right press brake tooling?
Yes. Send us your machine model, existing tooling, workpiece drawing or bending requirements. Our engineers can help recommend a suitable punch, die or custom tooling solution.
Continue Your Bending Journey
Product Details
Learn more about this tooling, specifications and compatibility.
→ Explore the Product: Standard Punch
Related Solutions
See related applications, bending methods and tooling discussions.
→ Explore Solutions & Discussions
Need a Price?
Tell us your requirements and get a tooling recommendation and quotation.
→ Request a Quote: Talk to Our Tooling Engineers
Continue the Bendmax Tooling Series
Next:
When Bending Space Gets Narrow, Sash Punches Find the Way
In the next article, we will move from deep-profile clearance to narrow bending access and introduce the Sash Punch.
Also known as a narrow type of Standard Punch, the Sash Punch features a slim body and an angled, inward-facing tip. This geometry helps the tool reach restricted bending areas where a conventional punch may interfere with the workpiece.
We will explore its structure, typical applications and differences from Standard and Gooseneck Punches, especially in door frames, window frames, sash profiles and narrow sheet metal sections.


 Phone: (0086)-15002165198
 Email: jason@bendmax.com
 Wechat: Privacy Policy

 IPv6 network supported
 English


